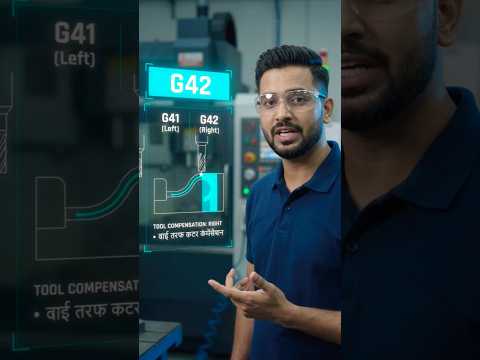
Achieving absolute precision in modern manufacturing requires a deep understanding of G-code programming. When operating advanced CNC machinery, commands like G41 and G42 play a vital role in ensuring your finished parts match exact design specifications. These two compensation codes allow machine operators to account for cutting tool radius without manually altering the geometry in the CAD/CAM software.
What is G41 (Cutter Compensation Left)?
The G41 code activates cutter radius compensation to the left of the tool path relative to the direction of tool travel. When the tool moves forward along a programmed contour, G41 shifts the tool center point to the left side of the part profile by the exact radius value stored in the controller's offset table. This compensation is most commonly used in climb milling operations, providing a cleaner surface finish and extending tool life.
What is G42 (Cutter Compensation Right)?
Conversely, the G42 code shifts the cutter radius compensation to the right relative to the direction of tool movement. When you program a tool path using G42, the center of the cutter offsets to the right side of the contour. This command is typically utilized during conventional milling processes where the cutting edge rotates against the direction of the feed.
Why Cutter Compensation Matters for CNC Machinery
Using G41 and G42 provides significant practical advantages when programming and running CNC machinery on the shop floor:
- Tool Wear Adjustment: As cutting tools wear down over time, operators can simply adjust the tool offset value in the control unit rather than rewriting the G-code program.
- Tool Substitution: It allows you to use undersized or reground end mills seamlessly without regenerating code from your CAM system.
- Dimensional Accuracy: Ensures strict tolerances and consistent part dimensions across high-volume production runs.
Essential Best Practices for G41 and G42
To prevent tool gouging or controller errors while operating CNC machinery, follow these key rules:
- Use Lead-in and Lead-out Moves: Always initiate compensation during a linear lead-in move that is longer than the cutter's radius.
- Cancel Compensation: Always use the G40 code to turn off cutter compensation before retracting the tool or making rapid positioning moves.
- Verify D-Offset Registers: Double-check that the correct D-offset register is called out alongside your G41 or G42 command to match the active tool.
By mastering G41 and G42, programmers and operators can maximize accuracy, reduce downtime, and unlock the full efficiency of their machinery.


